How thermal conductivity affects thermal management material prices
by
Published
Views:
Higher thermal conductivity can raise the price of a gap filler, thermally conductive adhesive, or battery potting compound, but it does not create a predictable price-per-W/m·K relationship. The premium depends on how the formulation achieves that conductivity—and whether the finished assembly benefits from it. A material rated at 6 W/m·K is not automatically twice as valuable as one rated at 3 W/m·K.
The useful comparison is cost per acceptable assembly at the required operating temperature, not simply price per kilogram or the highest conductivity on a datasheet. Filler chemistry, density, application thickness, contact quality, dispensing losses, and curing requirements can all change which quotation offers the lower production cost.
Why higher conductivity changes the cost structure
Polymer-based thermal management materials combine a resin system with thermally conductive fillers. The resin provides properties such as adhesion, flexibility, electrical insulation, and environmental resistance. The fillers establish pathways for heat transfer. Raising conductivity requires changes to those pathways, rather than simply adding a nominal performance feature.
One route is to increase filler loading. This raises the proportion of mineral or other conductive solids relative to the polymer. However, loading cannot increase indefinitely without affecting flow, wetting, flexibility, and processing. As particles become more crowded, maintaining a dispensable and stable formulation becomes more demanding.
Another route is to change filler chemistry, particle size distribution, shape, or surface treatment. These adjustments can improve heat-transfer pathways or allow more efficient particle packing. They can also add raw-material and processing costs.
Alumina, boron nitride, aluminum nitride, and metallic fillers provide different combinations of thermal, electrical, and processing properties. Their names alone do not establish a reliable finished-material price ranking. Filler grade, loading, formulation architecture, and purchase volume remain important. Metallic fillers also cannot be treated as straightforward substitutes where electrical insulation is mandatory.
The price relationship becomes especially application-specific when high conductivity must coexist with low viscosity, softness, adhesion, flame performance, or low assembly stress. A premium may therefore pay for a difficult combination of properties, not conductivity alone.
Determine how much conductivity the assembly actually needs
Bulk thermal conductivity describes heat transfer through the material. The assembly experiences thermal resistance, which also depends on geometry and interfaces. For a uniform layer with one-dimensional heat flow, the material contribution is:
Thermal resistance = layer thickness ÷ (thermal conductivity × contact area)
This simplified relationship provides a useful screening calculation. Consider a 1 mm layer covering 100 cm². At 2 W/m·K, its calculated bulk thermal resistance is 0.05 K/W. At 4 W/m·K, it is 0.025 K/W. Under a 100 W heat load, the corresponding temperature drops across the material are 5°C and 2.5°C.
These are illustrative calculations, not product test results. They exclude contact resistance, spreading resistance, voids, and other heat paths. Their commercial significance is that doubling conductivity saves only 2.5°C across this particular layer. Whether that saving warrants a premium depends on the available temperature margin.
If the lower-conductivity material already meets the temperature limit with sufficient allowance for manufacturing variation and aging, the higher grade may offer little purchasing value. If the assembly is close to its limit, the same temperature reduction may be decisive.
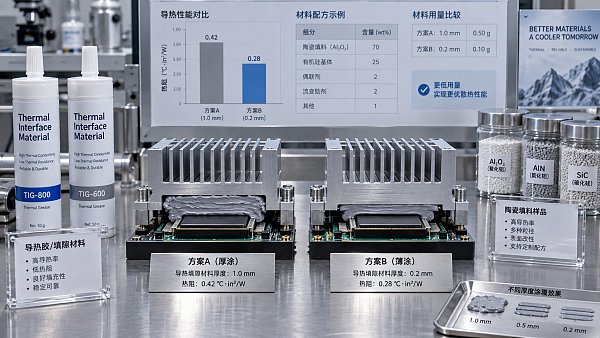
Thickness deserves equal attention. In the simplified calculation, halving layer thickness has the same effect on bulk resistance as doubling conductivity. A controlled, thinner adhesive bond line can therefore outperform a thicker layer with a higher conductivity rating. That is not permission to reduce thickness arbitrarily: gap tolerances, electrical isolation, surface flatness, and mechanical movement may establish a minimum.
Gap fillers illustrate the limitation clearly. Their purpose includes bridging dimensional variation. A specification based only on nominal gap size can understate the resistance at the largest production gap. Conductivity should be evaluated against the permitted gap range, not only the best-fitting prototype.
Make sure supplier conductivity values are comparable
A quotation comparison becomes unreliable when conductivity figures come from different test methods, temperatures, specimen conditions, or material orientations. A single W/m·K value does not disclose those differences.
For filled polymers, particle orientation can make through-plane conductivity different from in-plane conductivity. The relevant direction is the direction heat must travel in the assembly. This distinction matters when comparing materials containing platelet-shaped fillers or products whose manufacturing process creates alignment.
Request the test method and conditions, whether the specimen was cured, and whether the quoted figure is typical or a guaranteed acceptance limit. For compressible pads and interface materials, also establish the pressure and thickness used for thermal-impedance measurements. Results obtained under greater compression may not represent an assembly with limited clamping force.
ASTM D5470 is a recognized method for measuring thermal transmission properties of thermally conductive electrical insulation materials. However, citing a standard does not by itself make two datasheets directly comparable. Specimen preparation, contact conditions, and the reported result still need examination.
Where the purchase decision depends on a small thermal margin, application-level temperature or thermal-resistance testing is more useful than negotiating over nominal conductivity alone. The test should preserve the intended gap, surfaces, dispensing pattern, cure condition, and assembly pressure.
Convert price per kilogram into cost per filled volume
Many assemblies consume thermal material by volume, while suppliers quote it by mass. Higher filler loading can increase density, making a kilogram cover fewer assemblies. A modest price increase per kilogram can therefore conceal a larger increase per unit produced.
For a dispensed material, the basic calculation is:
Material cost per assembly = applied volume × mixed-material density × price per unit mass
Consider two hypothetical quotations for a 10 cm³ application. These figures are calculation examples, not market price benchmarks.
Material B costs 50% more per kilogram but 125% more for the same filled volume. It may still be justified by thermal performance or another required property, but the premium should be assessed as $0.20 per assembly—not merely a $4/kg difference.
For two-component materials, confirm that the quotation covers the complete mixed system and use mixed density. Check whether the mixing ratio is specified by weight or volume. For preformed pads, compare the cost per usable part at the required thickness, including cutting yield and any conversion charges.
Processing costs can outweigh the conductivity premium
A formulation that meets its thermal target but cannot run reliably on the intended equipment is not a lower-cost alternative. Highly filled materials can place greater demands on pumping, mixing, and dispensing, although filler content alone does not predict viscosity. Particle engineering and resin chemistry can substantially alter flow behavior.
Viscosity comparisons therefore need matching conditions. Temperature and shear rate matter, and a single datasheet value may not describe behavior during pumping, passage through a static mixer, or settling after dispensing. The relevant evidence is stable delivery at the required shot size and cycle time.
Conductivity-related formulation changes can introduce costs through:
- Dispensing pressure: different pumps, larger flow passages, or slower delivery may be needed.
- Equipment wear: abrasive fillers can affect seals, valves, and other wetted components.
- Mixing and purge losses: mixer volume, production interruptions, and usable working time determine discarded material.
- Air management: entrained air and incomplete wetting can undermine the expected thermal benefit.
- Curing requirements: heat, fixture time, and work-in-progress inventory can change conversion cost.
These effects should be established through trials rather than assumed from conductivity. A higher-priced formulation with better flow may reduce waste or avoid an equipment change. A cheaper material may require enough additional process control to reverse its apparent saving.
Usable yield belongs in the comparison. Material retained in containers, expired after opening, left in mixers, or consumed during startup still appears on the invoice. Cost per accepted assembly should include those losses as well as application labor, equipment time, and material-related rejects.
Keep non-thermal requirements fixed when comparing prices
A conductivity upgrade is not a valid substitute if it compromises another mandatory function. Thermally conductive adhesives must also meet bond and durability requirements. Battery potting compounds may need specified electrical insulation, mechanical compliance, flame performance, and compatibility with adjacent components. Gap fillers may need to limit compression force on sensitive parts.
These requirements explain why two materials with the same conductivity can have very different prices. A soft material that transfers heat without imposing excessive stress solves a different problem from a rigid adhesive that must carry structural loads. Comparing them on W/m·K alone creates a false equivalence.
Qualification evidence also has a defined scope. A flame classification or electrical test result should be checked against the exact grade, specimen thickness, cure condition, and applicable documentation. It should not be assumed to cover a related formulation merely because the product names are similar.
Set the purchasing specification around a thermal window
A defensible specification starts with the assembly temperature limit, heat load, gap range, and necessary non-thermal properties. It then establishes a conductivity or thermal-resistance requirement that meets those conditions with an appropriate margin. Specifying the highest available conductivity before this work locks unnecessary cost into the sourcing exercise.
Request quotations on a common basis: material form, required performance, annual volume, order quantity, packaging, shelf life on delivery, and delivery terms. Where conductivity drives the premium, ask suppliers to quote a compliant baseline and a higher-performance alternative with the differences identified. This exposes the incremental cost instead of burying it in unrelated formulation changes.
For shortlisted materials, compare delivered cost per usable volume, consumption per assembly, process losses, and qualification requirements. Agree on acceptance limits and change-notification obligations where formulation consistency is critical. A second source needs independent validation; matching conductivity does not establish equivalent processing or durability.
The appropriate thermal management materials price is the cost of meeting the assembly’s thermal requirement reliably. Pay the conductivity premium when it creates necessary temperature margin or enables a valuable design change. Where that benefit cannot be demonstrated, tighter control of thickness, contact, and dispensing may deliver more value than a higher W/m·K rating.
Recommended News
 Oct 16, 2026How thermal conductivity affects thermal management material pricesExplore thermal management materials price drivers, from conductivity and filler chemistry to processing costs. Learn how to meet thermal targets without overpaying.
 Sep 24, 2026What to ask a thermal management materials manufacturer before samplingThermal management materials manufacturer checklist: ask the right sampling questions on heat paths, process fit, reliability, and production support.
 Sep 22, 2026Thermal Interface Pastes Explained: Key Properties for Power Electronics CoolingThermal interface pastes for power electronics cooling: compare conductivity, dielectric safety, pump-out resistance, and dispensing performance for reliable designs.
 Sep 11, 2026What to verify before choosing an EV battery thermal management supplierEV battery thermal management supplier selection guide: verify thermal performance, electrical safety, process compatibility, validation data, and supply support.
 Aug 23, 2026How to qualify a thermal interface adhesives supplier for EV battery assemblyThermal interface adhesives supplier selection for EV battery assembly: learn how to assess thermal performance, dispensing stability, compliance, and scale-up support.
 Jul 25, 2026ECHA Adds Three Phthalates to SVHC ListECHA Adds Three Phthalates to SVHC List: learn how DEHP, BBP, and DBP impact REACH documents, SCIP filing, and EU customs compliance for thermal materials suppliers.
 Jul 24, 2026ECHA Adds 3 SVHCs, REACH Declarations for Thermal Pastes Must Be UpdatedECHA adds 3 SVHCs: learn why REACH declarations for thermal pastes must be updated, how SCIP and SDS rules affect EU exports, and what suppliers should check now.
 Jul 23, 2026ECHA Adds 3 SVHCs, Prompting REACH UpdatesECHA Adds 3 SVHCs, Prompting REACH Updates: learn how Thermal Conductive Pastes, Flame-retardant PU Potting, and EU exporters should respond within six months.
 Jul 22, 2026ECHA SVHC Update Triggers REACH Review for Thermal PastesThermal conductive pastes face urgent REACH review after the ECHA SVHC update. Learn how new Candidate List entries affect SDS updates, EU exports, and compliance readiness.
 Jul 21, 2026ECHA Adds 3 SVHCs, Raising REACH DemandsECHA adds 3 SVHCs to the Candidate List, raising REACH demands for EU-bound thermal interface materials and thermal conductive pastes. See key risks, SCIP duties, and compliance actions.
 Jul 20, 2026ECHA Updates SVHC List, Pressuring Thermal Paste ComplianceECHA updates the SVHC list, raising urgent REACH compliance pressure for Thermal Conductive Pastes in the EU. See key deadlines, supply chain risks, and actions for buyers and manufacturers.
 Jul 19, 2026How to Choose Thermal Interface Materials for EV BatteriesThermal interface materials for EV batteries: learn how to compare conductivity, insulation, gap control, safety, and process fit to choose reliable, high-performance solutions.
 Jul 15, 2026Battery Thermal Management Materials: Comparing Gap Fillers, Pads, and PastesBattery thermal management materials compared: gap fillers, pads, and pastes for EV packs. Learn how to balance heat transfer, manufacturability, cost, and reliability.
 Jul 12, 2026UL94 Thermal Interface Materials: What Ratings Mean for Device SafetyUL94 thermal interface materials explained: learn what V-0, V-1, V-2, and HB ratings mean for device safety, compliance, and smarter material selection.
 Jul 06, 2026Thermal Interface Adhesives Price: Cost Drivers and Spec Trade-OffsThermal interface adhesives price explained: compare cost drivers, spec trade-offs, hidden procurement costs, and sourcing tips to choose the right material with better total value.
 Jul 06, 2026Thermal Interface Materials for Consumer Electronics: What Affects Cooling Performance?Thermal interface materials for consumer electronics directly shape cooling, reliability, and device comfort. Discover what really affects TIM performance beyond conductivity.
 Jul 04, 2026Battery Heat Dissipation Materials: What Improves Cooling Without Adding WeightBattery heat dissipation materials that boost cooling without extra weight. Learn how TIMs, gap fillers, films, and graphite solutions improve battery safety, lifespan, and pack efficiency.
 Jun 30, 2026How to Compare Flame Retardant Thermal Management MaterialsFlame retardant thermal management materials comparison made practical: learn how to assess thermal paths, flame ratings, process fit, and long-term reliability for smarter material selection.
 Jun 23, 2026Battery Thermal Management for Automotive: Paste or Potting Compound?Battery thermal management for automotive: should you choose thermal paste or potting compound? Compare heat transfer, protection, rework, and production fit to make a smarter EV battery design decision.
 Jun 23, 2026Industrial Adhesive Market Trends for EV Battery Thermal MaterialsIndustrial adhesive market trends EV battery leaders watch now are reshaping thermal materials, dispensing, and compliance. Discover what drives safer, faster EV battery production.
 Jun 18, 2026UL94 Thermal Management Adhesives: How to Balance Heat and Flame RatingsUL94 thermal management adhesives explained: learn how to balance flame ratings, heat dissipation, dispensing stability, and long-term reliability for safer, smarter material selection.
 Jun 14, 2026Battery Adhesive Technology: Key Trade-Offs in Thermal Control, Safety, and ReworkBattery adhesive technology shapes thermal control, safety, and rework in EV battery packs. Explore key trade-offs, process risks, and smarter material choices for reliable production.
 Jun 13, 2026Thermally Conductive Adhesives: Key Selection Factors for Heat-Sensitive DesignsThermally conductive adhesives selection guide for heat-sensitive designs. Learn how conductivity, viscosity, cure, and substrate fit improve reliability and cooling.
 Jun 12, 2026Guangzhou Adhesives Show Signals Compliance-Focused BuyingGuangzhou Adhesives Show signals compliance-focused buying as overseas buyers prioritize thermal conductive pastes, UV curing adhesives, and silicone encapsulants with sample validation and technical documentation.
Editor's Selection
The Archive Newsletter
Critical industrial intelligence delivered every Tuesday. Peer-reviewed summaries of the week's most impactful logistics and market shifts.